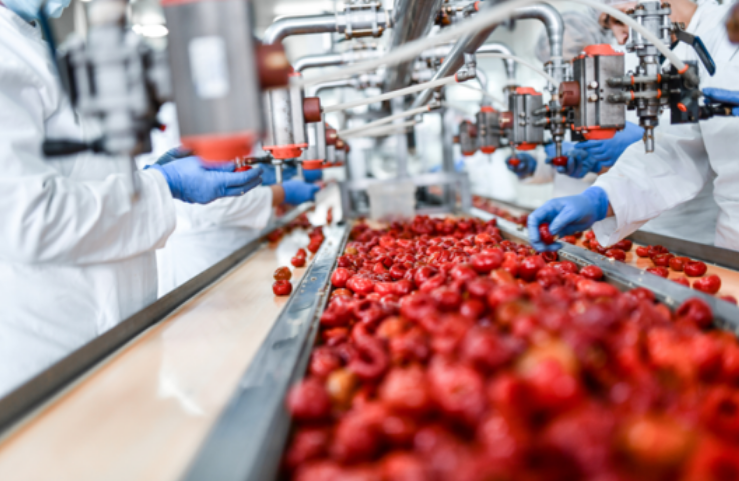
In the food processing industry, maintaining high standards of safety, sanitation, and efficiency is paramount. One often important part of this process is the rubber hose. Custom rubber hoses are indispensable for transporting various food products, cleaning solutions, and even air and gases within food processing plants. Tailor-made to meet stringent safety and sanitation standards, these hoses ensure that the quality of food products is maintained from start to finish.
This article explores the importance of custom rubber hoses in food processing and how they contribute to ensuring quality and compliance.
The Role of Rubber Hoses in Food Processing
Rubber hoses are used extensively in food processing for several key applications, including the transfer of liquids, solids, and gases. Their flexibility, durability, and resistance to a wide range of temperatures and chemicals make them ideal for various stages of food production. Here are some specific roles that rubber hoses play in the food processing industry:
Fluid Transfer: Custom rubber hoses are used to transfer liquids such as milk, juices, sauces, and syrups. These hoses must be food-grade to prevent contamination and ensure the safety of the products.
Cleaning and Sanitation: High-pressure rubber hoses are used for cleaning and sanitation processes within food processing plants. These hoses must withstand harsh chemicals and high temperatures to ensure thorough cleaning.
Product Handling: Rubber hoses are also used for handling dry products like flour, sugar, and grains. These hoses must be abrasion-resistant and designed to prevent the buildup of static electricity.
Steam and Air Transfer: In some food processing applications, steam and air are used for cooking, cleaning, and drying. Rubber hoses designed for these applications must be capable of withstanding high temperatures and pressure.
Customisation for Quality and Compliance
Custom rubber hoses are designed to meet the specific needs of different food processing applications, ensuring compliance with industry standards and regulations. This process involves selecting the appropriate materials, designing the hose to the required specifications, and incorporating features that enhance performance and safety.
Material Selection
The choice of materials is crucial in ensuring that the hose is food-grade and suitable for its intended use. Common materials include silicone, EPDM, and nitrile rubber, each with its unique properties and advantages.
Design Specifications
Custom hoses are designed to meet the specific requirements of the application, including size, length, flexibility, and pressure rating. This ensures that the hose fits perfectly within the system and performs optimally.
Special Features
Custom hoses can be equipped with features such as reinforcement layers, smooth inner linings to prevent product buildup, and anti-static properties to enhance safety and efficiency.
Meeting Safety and Sanitation Standards
The food processing industry is governed by strict safety and sanitation standards to ensure the quality and safety of food products. Custom rubber hoses play a crucial role in meeting these standards by providing reliable and safe solutions for various applications.
FDA Compliance
Food-grade rubber hoses must comply with FDA regulations to ensure that they are safe for use in food processing. This includes using materials that do not leach harmful substances into the food and ensuring that the hoses can be easily cleaned and sanitised.
Sanitary Design
Custom rubber hoses are designed with smooth, non-porous surfaces that prevent the buildup of bacteria and other contaminants. This ensures that the hoses can be easily cleaned, maintaining the hygiene of the food processing environment.
Enhancing Efficiency and Reliability
In addition to ensuring safety and compliance, custom rubber hoses enhance the efficiency and reliability of food processing operations. By providing solutions tailored to specific needs, these hoses help to minimize downtime, reduce maintenance costs, and improve overall productivity.
Durability
Custom rubber hoses are designed to withstand the harsh conditions of food processing environments, including exposure to chemicals, high temperatures, and abrasive materials. This durability ensures that the hoses have a long service life, reducing the need for frequent replacements.
Flexibility
The flexibility of rubber hoses allows them to be used in a variety of applications and environments. Custom hoses can be designed to bend and flex without kinking, ensuring smooth and uninterrupted flow.
L-Flex was established in 1993, manufacturing rubber hoses and providing technical services in product design. Over the years, we have been actively involved in the Rubber Industry in various disciplines and technical work studies. This has afforded us an experiential advantage in Material Handling and Product Application. We manufacture Rubber Hoses from sizes 25mm to 1000mm in diameter and also supply and manufacture products with a wide range of abrasive liners and sheeting.